
 EN
Quick Links
Last Updated:08/27/2026 Author: Zeon
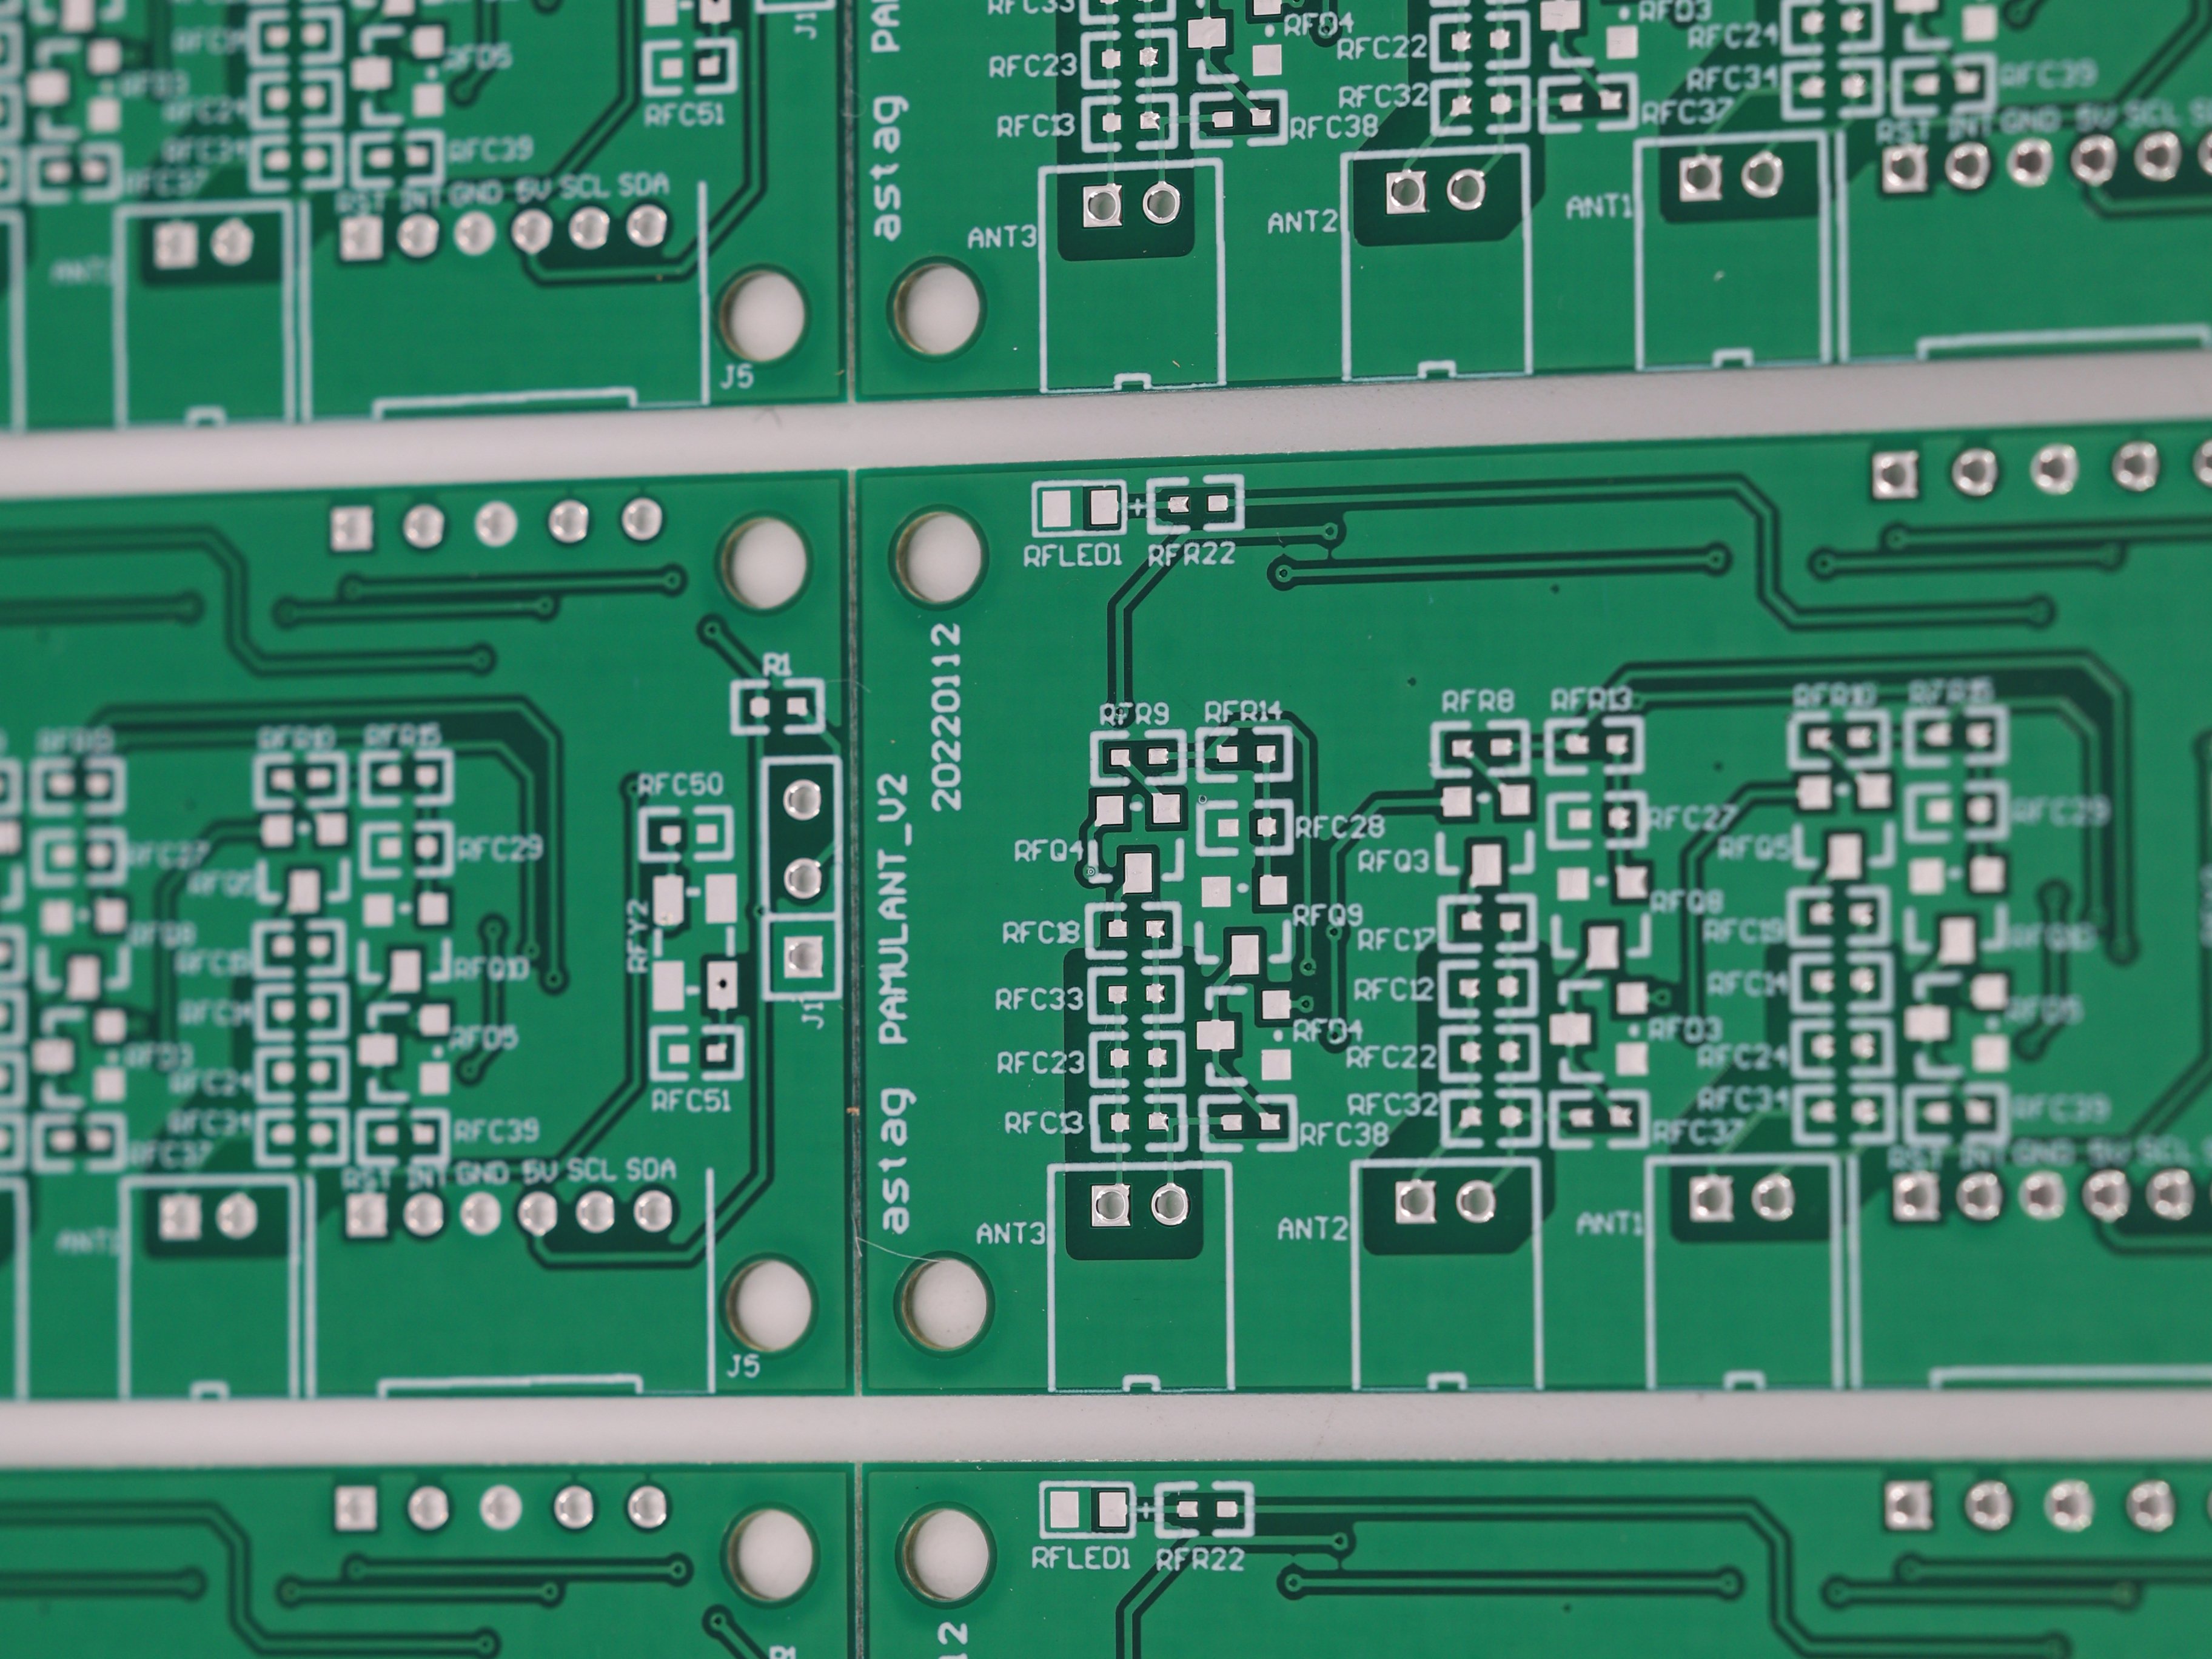
The box showed up with a cool tag: "IC-U3, Qty 12,000, Date Code 2024-W18." That was 18 months prior to the assembly day. Inside, the reels were still vacuum-sealed, the desiccant pouches undamaged, the inspection sticker labels untouched. The consumer's getting group had done every little thing right-- purchased early, stored carefully, documented extensively. Every little thing other than checking the day code against the schedule.
On the SMT line, the very first reel completed zero alarm systems. The reflow oven profile matched the paste datasheet. But when the boards appeared of assessment, the joints around U3 really did not look right. The solder had not moistened up the part leads. It sat there in rounded, dull spheres, refusing to climb the pins. X-ray validated what the eyes presumed: a row of head-in-pillow joints-- the BGA-style void between the round and the pad-- and loads of non-wetting connections that would certainly pass an informal glimpse and fail within a year.
Here's the second hook: this really did not occur since the customer purchased bitter pills. It took place because customer-supplied material-- the components your customer hands you to put together-- lugs a clock that begins ticking at the plating line, not at your dock. No one established the alarm. And when it sounds, it rings in your reflow oven, on your shift, against your return.
Customer-supplied material (CSM)-- likewise called customer-furnished material-- is the one course of input where the assembly residence has the least control and one of the most exposure. The components arrive from the client's stockroom, broker, or distributor. The assembly residence is in charge of the end result however not the procurement. That split creates an unseen area: purchase choices (for how long to hold stock, where to keep it, when to use it) are made by the client, while the repercussions come down on the production line.
And the failing mode is dangerous. Oxidized leads don't look damaged. A reel of tin-plated QFP leads from 2024 might look the same to one made last month-- slightly duller, maybe, if you're looking carefully, yet nothing that would fail an incoming inspection. The oxidation layer on the plating is gauged in nanometers. It's unseen to the eye, unseen to a digital microscopic lense, and completely adequate to quitted solder from wetting.
The surface of a modern part lead is a layer-- normally tin or tin-lead plating over a copper or alloy base. The plating exists for one reason: to provide a surface area that molten solder can bond to. Bare copper would certainly oxidize in hours. Tin oxidizes far more slowly-- however it does oxidize. Offered monts and ambient humidity, a layer of tin oxide forms on the surface area. Solder doesn't damp tin oxide. It moistens clean steel.
The clock on that procedure is the plating's life span, and the sector agreement is blunt: element solderability is normally ensured for 6 to one year from the plating day, with deterioration speeding up beyond 2 years. The warranty includes conditions-- closed packaging, regulated humidity, sensible temperature. Break any one of those and the clock accelerate. Store draws in a moist storage facility without desiccant and a 12-month part can lose solderability in 4.
There's a 2nd, associated failure that compounds the trouble: moisture absorption. Numerous IC bundles are moisture-sensitive (MSL-rated). Elements stored in damp problems take in water into the mold substance. At reflow temperatures-- normally 240-260 ° C for lead-free-- that water flashes to steam instantaneously, and the plan can crack from the inside out, an issue known as popcorning. The leads may damp flawlessly. The package is still ruined. For customer-supplied parts stored long-lasting, oxidation and wetness absorption typically show up with each other, and they generate failures that look entirely various however trace to the very same source: time invested in uncontrolled storage.
When an oxidized lead satisfies liquified solder in the reflow oven, the physics is unforgiving. Moistening requires the solder to form an intermetallic bond with the base metal-- that indicates liquifying with the surface area oxide to get to tidy metal. The flux in the solder paste is meant to do that task, chemically removing the oxide. But change has limited capability. A normal quantity of oxide is taken in quickly. A hefty oxide layer from 18 months of storage can wear down the flux before the surface area is tidy, leaving the solder with absolutely nothing to bond to.
The noticeable outcomes can be found in three flavors, all recorded in the IPC handiwork criteria:
Non-wetting-- the solder touches the lead yet never sticks. The joint resemble solder sitting on glass. It might pass a visual check if the geometry hides it, and it will stop working electrically at the most awful possible minute.
Dewetting-- the solder at first moistens, then pulls back into grains as the oxide re-forms underneath it. The result is a joint with partial protection and substantially decreased toughness. Dewetting is the classic trademark of a marginal, borderline-oxidized surface.
Head-in-pillow-- the round on a BGA or the solder on the pad never ever combines with the component lead's solderable surface. You wind up with 2 separate solder masses that look attached in X-ray and are hardly touching actually. Head-in-pillow is the most harmful of the three, since it's the hardest to spot and one of the most likely to trigger recurring area failures.
This is where the CSM problem obtains structurally unreasonable to the assembly house. Criterion incoming assessment checks amount, packaging, date codes, and visual problem. None of those find oxide layers. A specialized solderability examination-- the dip-and-look technique or moistening equilibrium per J-STD-002-- would certainly capture it, yet that examination is damaging, takes time, and is hardly ever operated on customer-supplied great deals unless there's currently a problem.
Even a full solderability examination on a sample has a statistical limitation. Oxide growth is not uniform throughout a reel or throughout a set. The edge of a reel that was revealed to air damps improperly; the center, shielded by nearby parts, moistens penalty. A sample of five parts can pass while the remainder of the lot fails. You're not evaluating the great deal. You're evaluating the five parts you chose.
When the issue turns up, the very first inquiry is always "whose mistake?" The customer's design group points at the assembly procedure-- the account, the paste, the handling. The assembly residence factors at the material. Both are partly right, and neither has clean hands.
The straightforward response is that responsibility ought to have been assigned before the reels struck the line, in writing. The industry-standard means to manage this: the assembly home executes and documents a solderability check on customer-supplied material at invoice, flags day codes beyond the 12-month window, and gets the customer's written acknowledgment that aging components will certainly be assembled at their danger-- or that aging components will certainly be rejected prior to assembly. That solitary step moves the argument from "you ruined my components" to "the components were understood to be at risk, and we settled on exactly how to handle it."
None of this is unique. The playbook is short and proven:
Display at receipt. Examine date codes versus the 12-month solderability home window. Run a dip-and-look or moistening equilibrium examination on a sample of any kind of whole lot older than 6 months. It takes an hour and it captures the disasters.
Store customer-supplied components like they're your own. Secured draw in a dry cupboard at controlled humidity. If the client's components show up in opened up or unsealed product packaging, flag it in writing. Moisture control costs dimes per reel and protects agains both oxidation and moisture-related bundle damages.
Bake for wetness, except oxide. Cooking an MSL-rated plan removes absorbed dampness and stops popcorning-- that part is actual. Cooking does not bring back solderability. An oxidized lead is an oxidized lead, and no quantity of heat reverses the chemistry. Groups that perplex both wind up cooking 18-month-old components, proclaiming them excellent, and seing the very same wetting failures appear on the line.
Agree on the danger before assembly, not after. The order or the setting up contract need to mention what takes place when customer-supplied product fails solderability screening: being rejected and return, setting up at customer risk, or re-tinning at customer cost. Written in advancement, it's a process note. Written after a stopped working set, it's a legal conflict.
Customer-supplied material is the one area in PCB assembly where the laws of chemistry and the terms of an agreement intersect. The chemistry is ruthless: a nanometer of oxide, undetectable and harmless-looking, stops solder dead. The agreement is optional-- nothing pressures any person to check a date code, run a wetting examination, or put the risk in composing.
The makers that prevent this failure aren't the ones with far better stoves or far better paste. They're the ones who treat a day code as a due date instead of a label. The clock starts at the plating line the day the component is ended up. It does not stop briefly for vacuum cleaner seals, purchase orders, or excellent purposes. Inspect it before the reel takes place the line-- or clarify to the consumer why their 18-month-old parts failed at your reflow oven, not their own.

Article written by Zeon
Hi, I'm Zeon — 20 years in PCB and electronics manufacturing. Front-end design and R&D, components sourcing, precision SMT, DIP through-hole assembly, and complete unit assembly. That's the full path from concept to finished product, and it's the path I've walked for two decades.
 Hot News
2026-09-17
2026-09-09
2026-09-07
2026-09-04
2026-09-03
2026-09-01
2026-08-31
2026-08-27








